The problem as it presented itself
The customer arrived with a working prototype and a production problem: the LEDs that passed the bench test were not the ones that survived the line. Nothing in the data was out of spec — the failures were spread across batches rather than concentrated in one lot, which ruled out a supplier problem and pointed at the process instead.
Three measurements separated the causes. First, forward voltage at a fixed low current across a sample of each batch, which showed whether the die set was consistent. Second, case temperature under the real drive condition, which showed whether the thermal path matched the assumption in the design. Third, the reflow profile logged on the line, which showed whether the assembly process stayed inside the qualified window.
The first two came back clean. The profile log showed the peak temperature sitting close enough to the limit that normal line-to-line variation pushed parts past it. This is the most common way a qualified component becomes an unqualified assembly, and it is invisible on the datasheet.
- Measure the process, not just the part. A component that meets its specification can still be assembled outside its qualification.
- Log the profile, do not assume it. Reflow profiles drift as boards and fixtures change.
- Look at failure distribution first. Failures spread across batches point at the process; failures concentrated in one batch point at the supply.
Once the profile was corrected and re-qualified, the field return rate dropped to the level the component datasheet predicts. The component never changed — only the process around it.
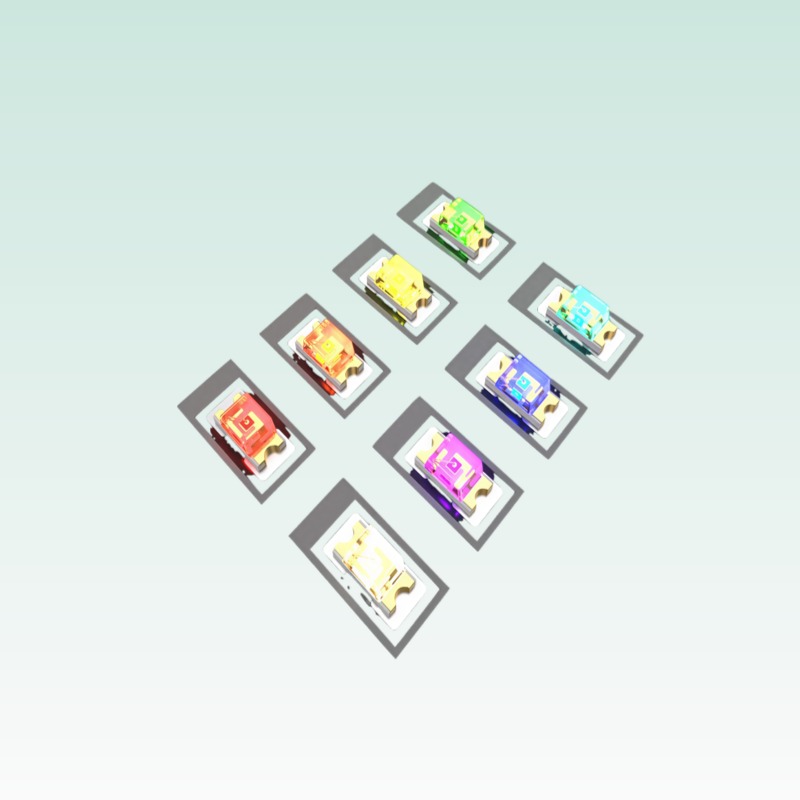
An industrial automation manufacturer required SMD 0805 indicator LEDs for PLC output modules and HMI panels. The indicators needed clear status visibility under factory lighting, withstand Pb-free reflow soldering, and maintain reliability over 100,000+ power cycles.
Queendom Solution
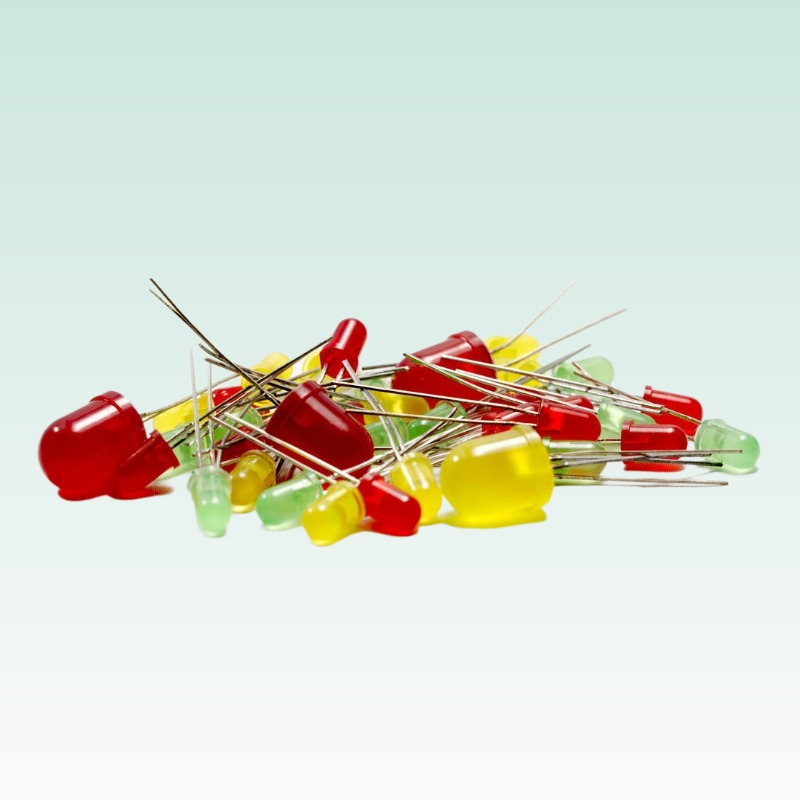
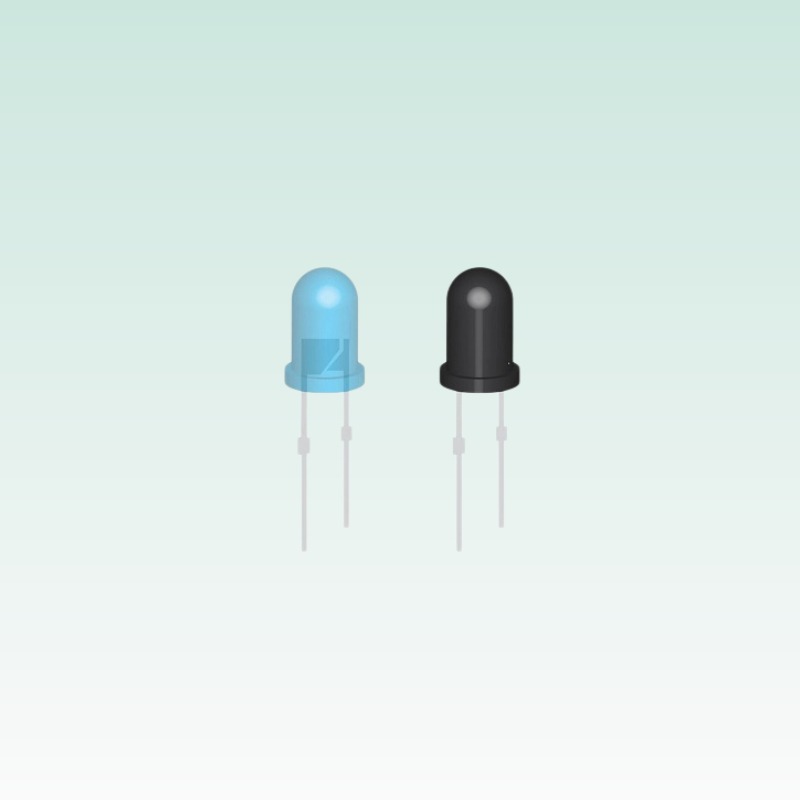
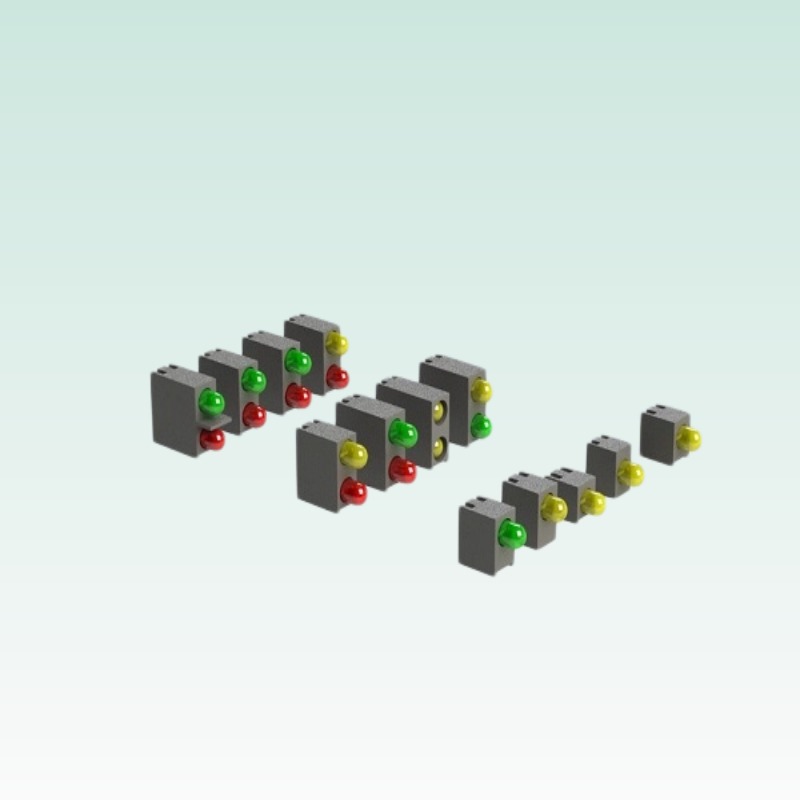
Queendom supplied through-hole board-mount indicator LEDs in T-1 3/4 (5mm) and T-1 (3mm) packages for PLC status indication panels. Available in red, green, yellow, blue, and white with water-clear or diffused lenses, these LEDs provide reliable visual status indication for industrial automation PLC systems. The wide operating temperature range and high ESD resistance ensure stable performance in harsh industrial environments.
Key Advantages:
- SMD 0805: Compact footprint for dense PCB arrays
- Luminous intensity: 5-15 mcd at 20mA
- Viewing angle: 120 diffused
- Reflow: Pb-free 260C (JEDEC J-STD-020)
- Reliability: 100,000+ power cycles, -40C to +85C
Product Specifications
| Parameter | Specification |
|---|---|
| Package Type | Through-hole Board Mount (T-1 3/4, 5mm / T-1, 3mm) |
| Colors Available | Red / Green / Yellow / Blue / White / Orange |
| Luminous Intensity | 50 – 2,000 mcd @ 20mA |
| Viewing Angle | 30 / 45 / 60 / 120 degrees (diffused/water clear) |
| Forward Voltage | 1.8V – 3.2V (color dependent) |
| Forward Current | 20mA (max 30mA peak) |
| Operating Temp | -40C to +85C |
| Mounting | Through-hole PCB mount, 2.54mm pitch |
| Certifications | CE / RoHS / REACH |
Application Scenarios
PLC Output Module
8-channel digital output, status indicators
HMI Panel
Multi-color status array, 24V DC operation
Equipment Dashboard
Fault/warning/run indicators, 100,000+ cycles
Case Direction
Industrial automation: SMD 0805 indicator LEDs for PLC modules, 500K annual volume, AEC-Q200 qualified for harsh environments.
Related Links
Solution: Industrial Indicator LEDs Solutions
Product: SMD LED Products
Case Studies: PCBA LED Case | Traffic LED Case
Discover how Queendom LED solutions can transform your application.
Contact UsPart of ← LEDs Case Studies
Related pages
- Infrared LEDs for Perimeter CCTV Illumination
- Narrowband UVB LEDs for Phototherapy Equipment
- Ceramic 3535 LEDs for Automotive Signaling
- SWIR LEDs for Semiconductor Wafer Inspection
- SWIR LEDs for Plastic Recycling Sorting
- UVC LED Water Treatment & Disinfection
…and 20 more in LEDs Case Studies.