 English
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Chichewa
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Filipino
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Hmong
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Korean
 Kurdish (Kurmanji)
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malagasy
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar (Burmese)
 Nepali
 Norwegian
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sudanese
 Swahili
 Swedish
 Tajik
 Tamil
 Telugu
 Thai
 Turkish
 Ukrainian
 Urdu
 Uzbek
 Vietnamese
 Welsh
 Xhosa
 Yiddish
 Yoruba
 Zulu
DIP LED Failure Analysis
Root-cause diagnosis and prevention for through-hole DIP LED failures in industrial panels, power supplies, and legacy equipment — covering lead corrosion, moisture ingression, wire bond failures, and thermal stress cracking.
1. Overview of DIP LED Failure Modes
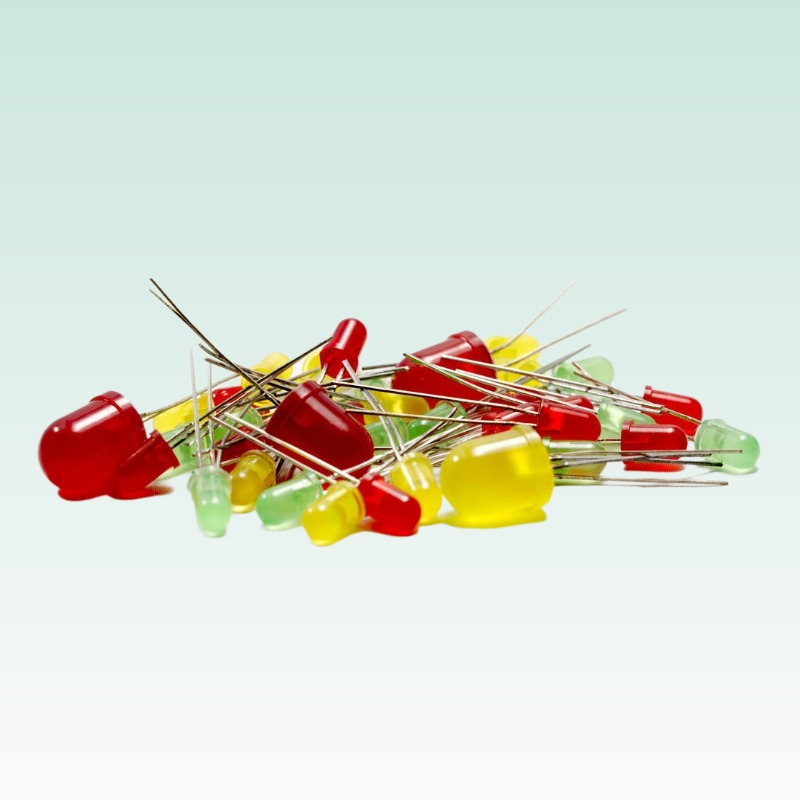
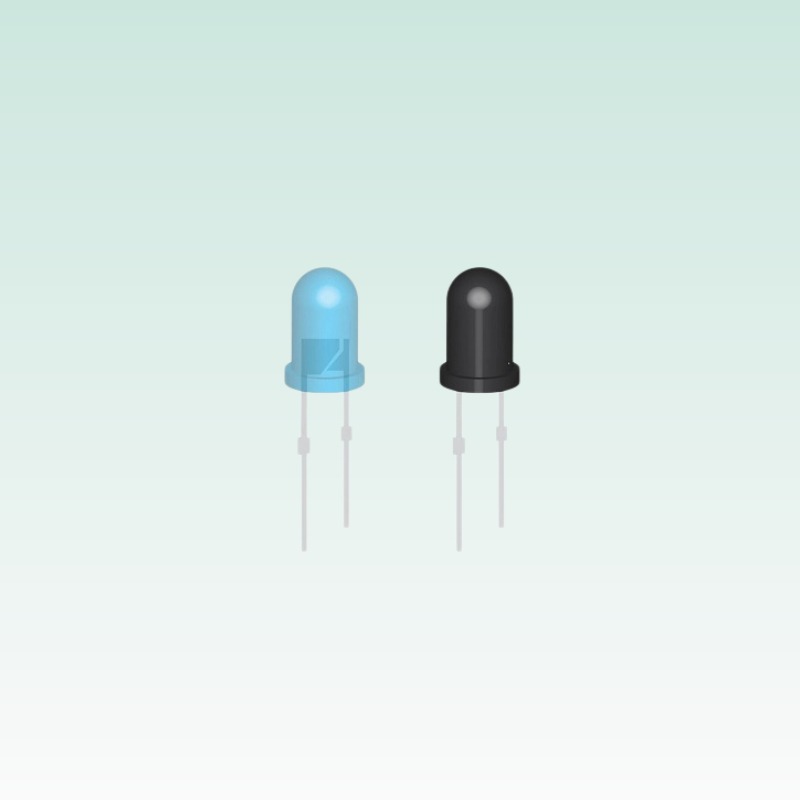
Through-hole DIP (Dual In-line Package) LEDs — including the ubiquitous 3mm (T-1) and 5mm (T-1 3/4) packages — remain widely used in industrial control panels, power supplies, automotive dashboards, and legacy equipment. Despite the industry trend toward SMD packages, DIP LEDs offer advantages in specific applications: they provide better mechanical stability in manual soldering processes, offer higher optical efficiency per individual package in indicator applications, and are easier to field-replace in maintenance scenarios.
However, DIP LED failure modes differ significantly from SMD packages because of their through-hole construction, leadframe design, and epoxy encapsulation process. Understanding these failure mechanisms is essential for engineers maintaining legacy systems, designing new through-hole assemblies, or specifying DIP LEDs for industrial environments.
| Failure Mode | Primary Cause | Typical Onset | Field Frequency |
|---|---|---|---|
| Lead Corrosion | Galvanic corrosion at lead-epoxy interface | 3–7 years | ~35% |
| Wire Bond Break | Thermal stress, mechanical shock | Any time | ~25% |
| Epoxy Degradation | UV exposure, thermal aging | 5–10 years | ~20% |
| Moisture Ingession | Hermetic seal breach at lead-epoxy interface | 2–5 years | ~12% |
| Die Attach Failure | Silver epoxy degradation, CTE mismatch | 4–8 years | ~8% |
2. Lead Corrosion and Leadframe Degradation
Lead corrosion is the most common DIP LED failure mode in industrial environments, particularly in applications exposed to humidity, sulfur compounds, or salt spray. The failure mechanism involves galvanic corrosion at the interface between the LED leadframe (typically silver-plated copper or FeNi42 alloy) and the epoxy encapsulation. Over time, moisture penetrates the lead-epoxy interface, creating an electrochemical cell that corrodes the leadframe material.
2.1 Corrosion Mechanism
The corrosion process begins with the gradual breakdown of the adhesion between the epoxy resin and the leadframe metal. This interface is the primary moisture barrier in DIP LED packages, and unlike hermetically sealed metal packages, it relies entirely on chemical adhesion. Factors that accelerate interface degradation include:
- Elevated operating temperatures (thermal cycling stress on the interface)
- High relative humidity environments (>75% RH sustained)
- Atmospheric pollutants: sulfur dioxide (SO2), hydrogen sulfide (H2S), chlorine compounds
- Mechanical stress from PCB flexure or vibration transmitted through the leads
Once moisture breaches the interface, corrosion propagates along the leadframe inside the package, eventually reaching the die attach area or wire bond. At this point, the electrical connection is compromised, leading to open-circuit failure or high-resistance intermittent operation.
2.2 Sulfur-Induced Corrosion
In industrial environments such as paper mills, wastewater treatment plants, and rubber manufacturing facilities, airborne sulfur compounds (particularly H2S) can cause rapid corrosion of silver-containing leadframes. Silver reacts with sulfur to form silver sulfide (Ag2S), which has a resistivity of 10,000 ohm-cm — effectively an insulator. This “silver migration” phenomenon can increase contact resistance by several orders of magnitude within months of exposure.
Prevention: For sulfur-containing environments, specify DIP LEDs with gold-plated leadframes (minimum 0.1 micron gold thickness) rather than silver-plated. Alternatively, use SMD packages with metal-core PCB construction, which provide better environmental protection. Apply conformal coating (silicone or polyurethane type) to the assembled board for additional moisture and chemical barrier protection.
3. Wire Bond Failures
Wire bonding is the electrical interconnection method used in virtually all DIP LEDs, typically using 1.0 mil (25 micron) gold wire from the LED die pad to the leadframe post. Wire bond failures account for approximately 25% of DIP LED field failures and can occur at any point in the product lifecycle.
3.1 Heel Crack Failure
The most common wire bond failure mode in DIP LEDs is heel cracking, where fatigue cracks initiate at the heel of the bond (the transition point between the wire and the bonded interface). This failure is caused by mechanical stress transmitted through the package, including thermal expansion mismatch between the wire (gold, CTE ~14.2 ppm/°C), leadframe (copper, CTE ~17 ppm/°C), and epoxy encapsulant (CTE ~15–25 ppm/°C below Tg, 60+ ppm/°C above Tg).
Heel crack failures are particularly common in applications where the LED is subjected to frequent temperature cycling, such as outdoor equipment exposed to day/night temperature swings, or indoor equipment with duty cycling. The crack propagates slowly through the gold wire cross-section, initially causing intermittent operation that may be misdiagnosed as a solder joint problem, and eventually leading to complete open-circuit failure.
3.2 Wire Sweep During Encapsulation
During the epoxy encapsulation process (transfer molding), the viscous epoxy can exert lateral force on the wire bonds, causing them to deform or “sweep” from their original position. Excessive wire sweep can bring the wire dangerously close to the leadframe, creating a short-circuit risk, or can stress the bond heel, creating a pre-existing crack that propagates during field use. This is a manufacturing defect that should be detected through destructive physical analysis (DPA) sampling per JEDEC JESD-22-A117.
4. Epoxy Encapsulant Degradation
The epoxy encapsulant in DIP LEDs serves three critical functions: mechanical protection of the die and wire bond, optical coupling of the LED emission, and environmental isolation. Degradation of any of these functions leads to LED failure or performance degradation.
4.1 UV-Induced Yellowing
DIP LEDs used in outdoor applications or near UV sources (such as UV sterilization equipment) experience photodegradation of the epoxy resin. The aromatic rings in standard epoxy encapsulants (typically bisphenol-A type) absorb UV radiation, causing chain scission and oxidation that manifests as visible yellowing. Yellowing reduces light output (particularly for blue and white LEDs, where yellowing absorbs the short-wavelength emission) and shifts the chromaticity coordinates.
For applications requiring long-term UV exposure, specify LEDs with silicone encapsulants, which are inherently UV-resistant. Silicone encapsulants also have better thermal stability (up to 200°C continuous operating temperature) and lower stress on the die due to their lower elastic modulus.
4.2 Thermal Aging
Even in indoor applications, prolonged operation at elevated temperatures causes gradual cross-linking and embrittlement of the epoxy encapsulant. The glass transition temperature (Tg) of standard LED epoxy is approximately 130–140°C; operation near or above this temperature causes rapid mechanical property changes and can lead to package cracking or delamination from the leadframe.
5. Case Study: DIP LED Failure in Railway Signal Equipment
Application: 5mm red DIP LEDs used in trackside signal indicators on a metropolitan rail network
Failure Mode: Progressive luminous output degradation and eventual open-circuit failure occurring 3–5 years after installation
Root Cause Analysis: Failed LEDs were sectioned and examined under optical and electron microscopy. The primary failure mechanism was lead corrosion at the leadframe-epoxy interface, with secondary damage to the die attach from moisture ingression. Environmental testing of the installation site revealed sulfur dioxide concentrations of 0.05–0.12 ppm, well within the range that causes silver sulfide formation on silver-plated leadframes.
Solution: (1) Replaced standard silver-plated DIP LEDs with gold-plated leadframe versions specifically rated for industrial sulfur environments. (2) Added a silicone conformal coating (IPC-CC-830 compliant) to the assembled signal boards, providing an additional moisture and chemical barrier. (3) Implemented a 3-year preventive maintenance cycle for LED replacement. After these changes, field failure rates decreased from 4.2% per year to 0.3% per year over a 24-month observation period.
6. Selection and Prevention Guidelines
| Environment | Recommended DIP Type | Leadframe | Additional Protection |
|---|---|---|---|
| Indoor / Consumer | Standard epoxy DIP | Silver-plated | None required |
| Industrial / Humidity | Silicone encapsulant DIP | Gold-plated | Conformal coating AR/UR type |
| Outdoor / UV Exposure | Silicone encapsulant DIP | Gold-plated | Conformal coating SR type |
| Sulfur / Chemical | Hermetic or SMD alternative | Gold-plated thick | IP65+ enclosure, silicone coating |
7. FAQ
Q: What is the typical service life of a DIP LED in an indoor environment?
A: For standard 5mm DIP LEDs operated at 20 mA forward current in ambient temperatures below 50°C, the typical L70 lifetime is 50,000–80,000 hours. However, this assumes proper current regulation and adequate ventilation.
Q: Can degraded DIP LEDs be repaired or reconditioned?
A: DIP LEDs cannot be reconditioned once the encapsulant or leadframe has degraded. The only solution is replacement. In through-hole assemblies, DIP LEDs can be desoldered and replaced relatively easily compared to SMD packages.
Q: How can I identify sulfur-induced corrosion before complete failure?
A: Early signs include increased forward voltage at rated current (indicating rising contact resistance) and visible darkening or discoloration at the base of the LED package where the leads enter the epoxy. Periodic luminous output measurement is the most reliable detection method.
8. Related Resources
- SMD LED Failure Analysis — failure modes for surface-mount LED packages
- DIP LED Datasheets — specifications for 3mm, 5mm, and bi-color DIP packages
- DIP Bi-Color & RGB LED Datasheets — multi-color DIP package specifications
9. Comparative Reliability: DIP vs. SMD
Engineers often ask whether DIP or SMD LEDs are more reliable for specific applications. The answer depends on the environmental conditions and the specific failure modes that are most likely in that environment. DIP LEDs have superior mechanical robustness at the PCB level — their through-hole leads provide a much stronger mechanical bond to the PCB than SMD solder joints, making them more resistant to vibration, mechanical shock, and thermal cycling stress. This is why DIP LEDs remain the preferred choice for automotive dashboard indicators, industrial equipment with heavy vibration, and any application where the LED may be subjected to mechanical abuse.
However, DIP LEDs have inferior environmental protection compared to SMD packages. The leadframe-epoxy interface in DIP packages is a known weakness for moisture ingression and chemical corrosion, whereas SMD packages — particularly those with silicone encapsulants — provide superior moisture barrier performance. For outdoor, high-humidity, or chemically aggressive environments, SMD packages with appropriate IP-rated fixtures are the better choice despite their lower mechanical robustness at the PCB level.
From a thermal management perspective, SMD packages have a significant advantage. The thermal resistance of SMD packages ranges from 6–45 C/W depending on package type, compared to 100–200 C/W for DIP packages. This makes SMD packages essential for any application requiring more than 0.1W power dissipation per LED. DIP LEDs should be limited to indicator applications at 20–50 mA forward current, or outdoor display applications where the larger package size provides better light distribution optics.
In summary: choose DIP LEDs for mechanically demanding, low-power indicator applications. Choose SMD LEDs for power applications, environmentally demanding applications, and any new design where PCB space and thermal efficiency are priorities.