These are the questions our component engineering group answers most often, collected from quotations, incoming inspection reports and design reviews over the past year. Each answer is written to be actionable: where a number is required, the number is given, and where a test method applies, the method is named so it can be cited in a purchase specification.
1. Binning and part numbers
Q1. What do the bin codes on a reel label actually mean?
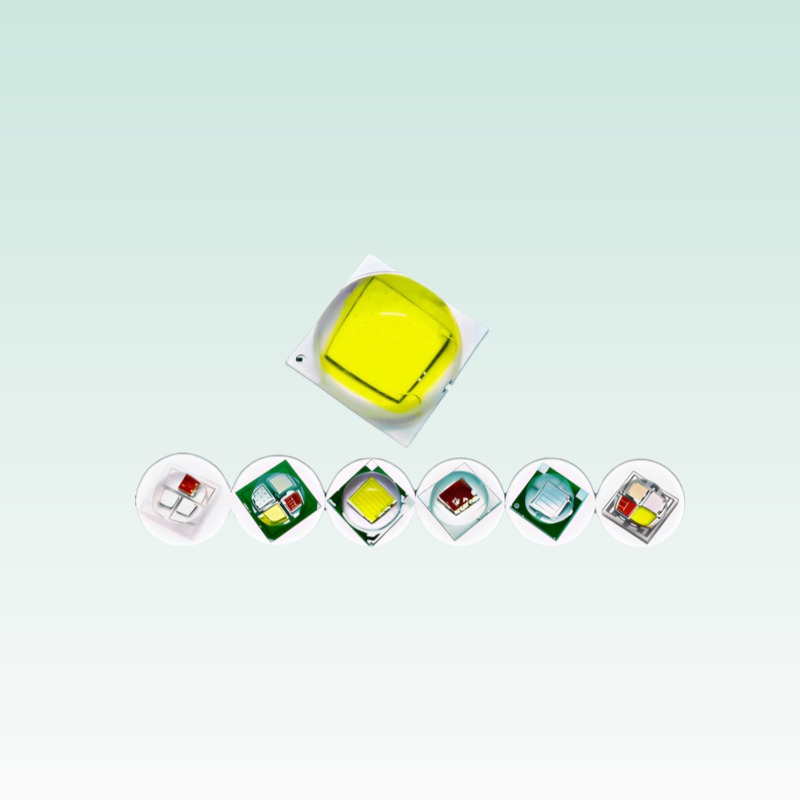
A white LED reel carries three independent bin codes. One describes luminous flux, one describes forward voltage and one describes chromaticity, usually as a quadrangle on the CIE 1931 diagram. The package size and the CRI grade appear separately. For example, a 3535 white part in the J-17 family might carry a flux bin letter, a voltage bin code and a three-step chromaticity quadrangle.
Q2. Can I mix two flux bins in the same fixture?
You can, and many suppliers do, but the fixture must then be specified with a tolerance rather than a nominal figure. Two adjacent flux bins differ by roughly 7 to 10 percent in output, which is visible in a side-by-side wall-wash installation and invisible in a single downlight. If the application is a continuous cove or a wall of panels, hold to one bin.
Q3. The quotation says “typical flux” but the reel does not match. Is that a defect?
No, if the specification named only a typical value. “Typical” is a distribution centre, not a limit. The reel is compliant if its bin code falls inside the window the specification allowed. This is the single most common first-article dispute, and it is resolved before the order by writing the bin code, or a named two-bin window, into the specification.
Q4. Why is the lowest voltage bin sometimes unavailable?
Because it sits in the tail of the yield distribution. Production measurement produces a curve that peaks two bins above the minimum, so the lowest bin is a small fraction of the run and allocation pressure falls on it. Buyers who need a narrow voltage window for a fixed-voltage rail design should plan a longer lead time or move to a constant-current driver.
2. Thermal derating
Q5. The datasheet says 60 mA. Can I run 60 mA in my fixture?
Only if your junction temperature stays inside the derating curve at that current. The catalogue current is quoted at a reference solder point temperature, usually 25 degrees C, which almost no real fixture achieves. Re-rate the current from the derating curve for the actual solder point temperature and the actual board thermal resistance before committing the design.
Q6. How much does the board really matter?
Enough to change the answer by a factor of two. The chart above shows three configurations of effectively the same package: a 3535 ceramic on a metal core board, a 3528 SMD on FR4 with thermal vias, and the same 3528 on FR4 with no thermal relief. At 100 degrees C junction, the permitted currents differ by more than two to one.
Q7. What thermal resistance should I assume for a 3535 ceramic?
Between 8 and 15 K/W junction to solder point, depending on the die size and the die-attach material, with the lower figure applying to the larger ceramic packages. Add the board and heatsink path on top; the package figure alone is never the whole chain.
Q8. Does drive current change the colour?
Yes, mildly. A phosphor-converted white LED shifts its chromaticity as current rises because the blue pump and the phosphor conversion saturate at different rates. The shift is normally inside the declared bin for moderate overdrive and grows quickly beyond it. Where colour stability is contractual, test at the application current rather than reusing the binning condition.
Both charts in this section describe the same underlying tension. The chart above shows that the abundant bins are not the ones a cost-optimised design usually asks for, and the derating chart showed that the permissible current depends on the thermal path rather than on the catalogue figure. A specification that ignores either one will pass at the bench and fail in the field.
3. Electrical questions
| Question | Short answer | Detail |
|---|---|---|
| Can I drive an LED from a fixed 5 V rail with one resistor? | Yes, below about 20 mA per branch | Design against the highest expected forward voltage in the bin, not the typical value, or the current will overshoot on the low-voltage parts. |
| Do I need a reverse protection diode? | Only if reverse bias is possible | Most LEDs tolerate several volts of reverse bias but not the full supply rail. Add a diode where the driver can be connected backwards or where an inductive load can push the node negative. |
| What ESD rating should I require? | 2 kV HBM minimum | Standard SMD parts meet 2 kV human body model. Handling discipline to IEC 61340-5-1 matters more than the rating, because most ESD damage happens in manual assembly, not in the field. |
| Can I parallel two LEDs directly? | Not without care | Forward voltage mismatch pushes current into the lower-voltage part, which then runs hotter and drops further. Use one resistor per branch or a constant-current driver with per-string sensing. |
| Is PWM dimming safe for the LED? | Yes, within the current rating | The die sees the same peak current as steady drive. Keep the PWM frequency above 1 kHz to avoid audible and visible artefacts, and above 3 kHz where cameras are present. |
| Do I need a constant-current driver? | Above about four LEDs per branch, yes | A series resistor on a long string wastes a large share of the supply as heat and gives poor current matching across bins. |
4. Lifetime and reliability
| Thermal parameter | Typical value | Why it matters |
|---|---|---|
| Junction to solder point, 3535 ceramic | 8 to 15 K/W | The package part of the chain; the board and heatsink add to it. |
| Junction to solder point, 3528 SMD | 25 to 40 K/W | Plastic body and smaller thermal pad make this the dominant term on a poor board. |
| FR4 with thermal vias, 1.6 mm | 15 to 30 K/W | Via count and copper area decide where in this range the board lands. |
| Aluminium metal core board | 3 to 8 K/W | The standard choice for any package run above 100 mA. |
| Heatsink to ambient, extruded | 1 to 4 K/W | Set by the fin area and the airflow, not by the extrusion profile alone. |
| Ambient rise in a sealed fixture | 10 to 25 K | Often overlooked; a sealed housing raises the effective ambient well above room temperature. |
| Question | Short answer | Detail |
|---|---|---|
| What does L70 mean and is it a warranty? | A projection, not a warranty | L70 is the projected hours at which output falls to 70 percent of initial, derived by TM-21 from LM-80 measurements. A warranty is a separate commercial commitment. |
| Why do two suppliers quote different L70 for the same bin? | Different test conditions | A projection at 55 degrees C case temperature and one at 85 degrees C are not comparable even when both are stated to the same hour count. |
| What is sulfurization and where does it appear? | Lead frame discolouration | Sulphur compounds in the ambient darken silver plating, raising contact resistance and reducing output. Rubber gaskets, some packaging and agricultural environments are the usual sources. |
| Do I need to bake parts before reflow? | Only past the floor time | Parts stored sealed within their moisture sensitivity floor time do not need baking. Parts left open past the floor time will popcorn at reflow. |
| How long will a part last at 10 degrees above the reference? | Materially less | Every ten degrees of extra junction temperature roughly halves many wear-out mechanisms. This is the single strongest argument for an oversized thermal path. |
| Does the driver affect the LED life? | Yes, strongly | Ripple current, inrush and a poor output capacitor all raise the effective junction temperature or stress the die. A marginal driver invalidates an otherwise good thermal design. |
5. Colour and optical questions
| Question | Short answer | Detail |
|---|---|---|
| Is CRI enough to specify colour quality? | No | The average over eight samples conceals the red rendering. Ask for R9 separately, and above 50 for retail and hospitality work. |
| What SDCM grade should I buy? | 3-step for retail, 5-step for general | A 3-step bin holds visible colour difference below the just-noticeable threshold across a continuous installation. |
| Will the colour drift over life? | Yes, slightly | Phosphor and die age at different rates, producing a small delta uv shift. Require a delta uv limit alongside the lumen maintenance figure. |
| Can one bin serve both 2700 K and 3000 K? | No | Those are different colour points and different quadrangles. A single bin cannot cover both without exceeding the visible colour difference. |
| How do I measure CCT in the field? | With a calibrated spectrometer | A colour meter that reports only CCT will not reveal the delta uv, which is the quantity that actually governs perceived colour shift. |
| Does the lens change the colour? | Only for diffused or tinted optics | A clear lens passes the spectrum unchanged. A tinted diffuser filters part of the spectrum and shifts both CCT and CRI. |
6. Incoming inspection
Q13. What should a goods-in check cover?
Four items. Verify the bin code on the reel label against the purchase order, sample the forward voltage against the declared bin, sample the flux against the declared bin, and check the chromaticity of a small sample against the declared quadrangle. The first item catches the majority of errors and takes two minutes.
Q14. How many parts should I sample?
For a normal inspection, five parts per reel for flux and forward voltage and three per shipment for chromaticity will catch a wrong bin with high confidence, because a wrong bin is a shift rather than a rare defect. Statistical sampling plans are unnecessary for a systematic error of this kind.
Q15. The sample matches but the field failures do not. What went wrong?
Usually the application condition, not the part. Field failures trace back to junction temperature in the great majority of cases: an underestimate of board thermal resistance, an ambient warmer than assumed, or a drive current taken from the catalogue rather than the derating curve. Return the failed parts for teardown before changing the supplier.
7. Part numbers in this FAQ
DIP and through-hole families appear in the J-10 to J-15 group, standard SMD packages in J-01 to J-09, multi-colour and addressable SMD in the J-16 to J-19 group, and high-power ceramic packages in a separate high-power range. The UV emitter family sits in its own group because the 275 nm to 405 nm range carries additional safety and material requirements. Where a question above depends on the exact part number, quote the full code including the bin so that the answer can be specific.
8. Related resources and next steps
For the vocabulary behind these answers, see the LED package and reliability glossary. For the electrical arithmetic behind the resistor questions, see the series resistor and array calculator. For a review of a specific design, send the part number, the board construction, the ambient temperature and the drive current, and our component engineering group will return a written derating check.
Electrical Design Questions
Six symptoms cover most field reports:
| Symptom | Likely cause | First check |
|---|---|---|
| LED dark, reads short | EOS or bond failure | Inspect bond, measure Vf at low current |
| LED dark, reads open | Wire-bond fatigue or severe ESD | Cycle-test a sample, X-ray the bond |
| Strip dim from one end | Parallel strings sharing one resistor | Measure per-branch current |
| Flicker under load | Driver instability or ripple | Scope the rail at the LED terminals |
| Color drift over months | Phosphor aging or sulfurization | UV lamp inspection of the package |
| Current rises as fixture warms | Negative Vf coefficient, weak regulation | Re-check headroom and resistor power |
Q12. Can I parallel LED strings without separate resistors?
No. A shared resistor lets the string with the lowest forward voltage draw the majority of the current. Give every branch its own resistor, or drive each branch from a constant-current output.
Q13. Why do identical parts from different bins change my current?
The bin window moves Vf by up to ±0.2 V. On a 5 V rail that is a ±40 percent swing in resistor current; on 24 V with three LEDs in series it stays under ±10 percent. Rail voltage is the lever you control.
Q14. Resistor or constant-current driver?
Resistors are right for indicators and low-current decorative loads. Above roughly 50 mA per branch, or wherever flux accuracy matters, a constant-current output costs less than the yield you lose to binning.
Handling and Storage Questions
MSL rules look like paperwork until a reel sits out overnight; the levels below are what most SMD LED datasheets specify.
| MSL level | Floor life at 30 C / 60 %RH | Bake before reflow |
|---|---|---|
| MSL 1 | Unlimited | Not required |
| MSL 2 | 1 year | 24 h at 125 C if exceeded |
| MSL 3 | 168 hours | 24 h at 125 C if exceeded |
| MSL 4 | 72 hours | 48 h at 125 C if exceeded |
Q15. Do SMD LEDs really need baking?
Only when the floor life is exceeded. The moisture concern is the lead-frame to molding-compound interface; popcorning during reflow appears later as delamination, not as an immediate electrical fault.
Q16. What ESD rating do catalogue SMD LEDs carry?
Typically 2 kV HBM (JESD22-A114 class 2) and 500 V CDM. That covers disciplined handling, not an ungrounded assembly line; wrist straps and grounded tips remain mandatory.
Q17. How long can a sealed reel stay in the bag?
Sealed with desiccant and a humidity indicator, storage life is commonly 12 months from the date of manufacture. Check the date code and the HIC card when the bag is finally opened.