Automotive component projects carry a documentation and qualification burden that general lighting projects do not, and the questions arrive in a predictable order: what the qualification standard requires, what evidence a supplier can provide, how the part behaves outside the reference condition, and what happens when something fails in the field. These are the questions we handle most often on automotive LED enquiries, with the standards named so that a quotation can be checked against a specification.
1. Qualification standards and scope
Q1. What is AEC-Q102 and what does it cover?
AEC-Q102 is the stress test qualification for discrete optoelectronic semiconductor components. It defines the test list, the sample sizes and the acceptance criteria for the part itself. It does not cover the module or the luminaire, which are qualified by the manufacturer against their own programme.
Q2. How does AEC-Q102 differ from AEC-Q101?
Q101 covers discrete semiconductors such as diodes and transistors; Q102 covers optoelectronic components such as LEDs and photodiodes. The test list overlaps substantially, but the optical measurements and the specific stress conditions differ because the failure modes of a light emitter are not those of a switching device.
Q3. Is AEC-Q102 enough for a tier-one customer?
No. It is a necessary qualification for the component, and it sits inside a wider programme that includes IATF 16949 quality management, PPAP documentation, traceability and often an ISO 16750 environmental validation at the module level. Expect to be asked for all of them.
Q4. What is PPAP and what level will be required?
PPAP is the production part approval process, and the level determines how much documentation accompanies each submission. Level 3 is the common default for a new part and includes the design record, dimensional results, material and performance test results, process flow, control plan and part submission warrant.
2. Thermal and electrical behaviour
Q5. Why is the automotive derating curve steeper?
Because the ambient range is far wider, the duty cycle is less predictable and the reliability expectation is measured in years at high availability. A general lighting derating curve assumes a benign indoor ambient for most of the operating life; an automotive curve must cover a bonnet-mounted fixture in summer sunlight.
Q6. What junction temperature should a design target?
Well below the absolute maximum, with margin for the worst-case ambient and the end-of-life thermal resistance. In practice, automotive programmes commonly target a junction temperature that leaves at least twenty degrees of margin to the absolute maximum at the worst-case ambient, and treat any design that relies on typical ambient as unqualified.
Q7. How does the forward voltage spread affect an automotive design?
It affects both the driver compliance range and the current matching across a string. Automotive designs commonly use a bin window narrower than the standard catalogue window, selected to keep the string current within tolerance without an active per-string regulator.
Q8. What ESD level is expected?
Higher than general lighting. Component-level human body model and charged device model ratings are both reported, and the assembly environment must be controlled to a defined level. Most field ESD damage in automotive modules occurs in handling and test, not in service.
3. Environmental and mechanical testing
| Test | What it exposes | Typical basis |
|---|---|---|
| Temperature cycling | Solder joint and die-attach fatigue from differential expansion | JESD22-A104 |
| High temperature operating life | Wear-out of the die and the encapsulant under continuous drive | JESD22-A108 |
| Thermal shock | Rapid transitions that cycling at a slower rate does not reproduce | JESD22-A106 |
| Humidity biased | Corrosion and ionic migration under electrical bias | JESD22-A101 |
| Vibration | Mechanical fatigue of wire bonds and solder joints | ISO 16750-3 at the module level |
| Mechanical shock | Handling and road impact events | ISO 16750-3 |
| Salt spray | Corrosion of the lead frame and the housing | ISO 9227 |
| Sulfurization | Silver-plated lead discolouration in a sulphur-bearing ambient | Internal qualification |
| Power temperature cycling | Cycling driven by the device’s own dissipation rather than by ambient | Used where the duty cycle dominates |
| Photometric stability | Colour and flux shift over the qualification duration | Measured against the initial condition |
4. Traceability and quality systems
| Derating input | Typical automotive value | Note |
|---|---|---|
| Maximum ambient, exterior forward lighting | 85 to 105 degrees C | Measured at the module location, not in the cabin. |
| Maximum ambient, exterior signalling | 85 to 105 degrees C | Similar to forward lighting; the duty cycle differs. |
| Maximum ambient, interior | 65 to 85 degrees C | Solar soak raises a parked cabin well above ambient air. |
| Junction temperature margin | At least 20 K below absolute maximum | Applied at the worst-case ambient, not the typical one. |
| Forward voltage bin window | Narrower than the catalogue window | Keeps string current within tolerance without an active regulator. |
| ESD, human body model | 2 kV or higher, reported | Charged device model is also reported for automotive programmes. |
| Qualification duration | Several thousand hours of stress testing | The programme timeline, not the test alone, is what a project plans around. |
| Question | Short answer | Detail |
|---|---|---|
| What traceability is required? | Lot level at minimum | A tier-one customer expects to trace a delivered part back to the wafer lot, the assembly lot and the test record. Marking and packaging must support that trace. |
| What quality system is expected? | IATF 16949 | ISO 9001 is a starting point and not sufficient on its own for an automotive programme. IATF 16949 adds the automotive-specific requirements and the customer-specific supplements. |
| Is a change notification required? | Yes, before the change ships | Automotive programmes normally require a PCN with a defined response window, because a silent process change invalidates the qualification evidence. |
| How is a deviation handled? | With a formal concession | An out-of-specification lot is not shipped on a verbal agreement. It needs a written deviation with a defined quantity, a defined expiry and a defined disposition. |
| What about sub-supplier control? | Named and audited | The qualification covers the whole bill of materials. A change of phosphor supplier or lead frame plating is a change of the qualified part. |
| How long must records be kept? | Typically the production period plus fifteen years | The exact retention requirement is set by the customer, and it is usually written into the quality agreement rather than assumed. |
5. Field performance and failure analysis
| Evidence item | What it demonstrates | Typical basis |
|---|---|---|
| AEC-Q102 test report | Component-level qualification against the optoelectronic stress list | AEC-Q102 |
| PPAP package | Production readiness and process control | Customer-specified level, commonly level 3 |
| Quality system certificate | Automotive-specific quality management | IATF 16949 |
| Material declaration | Compliance with restricted substance requirements | Customer and regulatory requirements |
| Reliability data at application conditions | Behaviour at the actual drive current and case temperature | LM-80 plus TM-21 projection, or a bespoke test |
| Traceability record | Link from the delivered lot back to the wafer and assembly lots | Lot-level marking and packaging |
| Change notification history | That the qualified part is the part still being shipped | PCN with a defined response window |
Q9. What are the most common automotive LED failure modes?
Three dominate. Solder joint fatigue from thermal cycling, encapsulant degradation from high junction temperature and UV exposure, and corrosion of the lead frame in a condensing or sulphur-bearing environment. Each traces back to a design or process choice rather than to the die itself.
Q10. How is a field failure investigated?
With an 8D process: contain the problem, characterise the failure, verify the root cause with a physical analysis, implement a corrective action, and verify that the action worked. The physical analysis typically includes X-ray inspection of the solder joints, cross-sectioning and a scanning electron microscope examination of the die attach.
Q11. What is the difference between a failure and a degradation?
A failure is a loss of function. A degradation is a measurable decline in performance that has not yet crossed the specification limit. Automotive programmes track both, and a steady degradation that will cross the limit within the warranty period is treated with the same urgency as a failure.
Q12. Can colour shift alone constitute a field failure?
Yes, where the specification includes a colour tolerance over life. A module whose colour drifts outside the declared tolerance is non-compliant even if it still produces light, and automotive specifications therefore usually carry a delta uv limit alongside the lumen maintenance requirement.
6. Project questions
Q13. What documentation comes with a qualified part?
The AEC-Q102 test report or the qualification summary, the PPAP package at the agreed level, the material declaration, the reliability data at the application condition where available, and the traceability record for the delivered lots. Where a part is in progress, the expected completion stage is stated in writing.
Q14. How long does qualification take?
The stress test sequence itself runs for several thousand hours, and the total programme including sample preparation, test, analysis and documentation typically spans many months. Projects that plan for a shorter window usually end up shipping on a deviation, which is the outcome the qualification programme exists to avoid.
Q15. What do you need from us to quote?
The application zone, the worst-case ambient, the expected duty cycle, the required qualification level and the documentation package expected by the customer. With those five inputs we can state whether a catalogue part is suitable, whether a sub-bin selection is required, and what the qualification timeline would be for a new part number.
7. Part numbers and programme scope
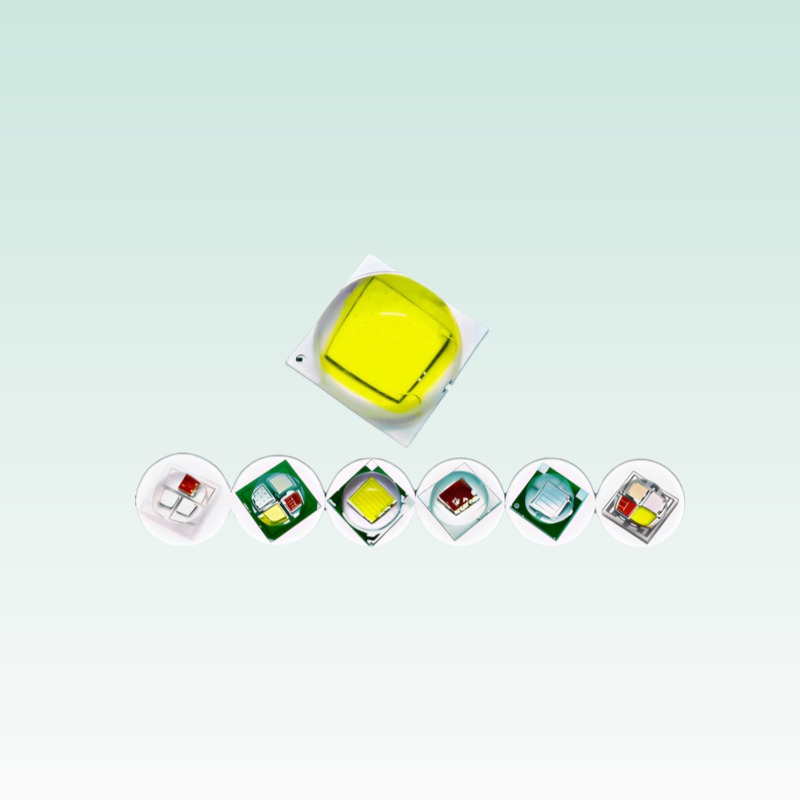
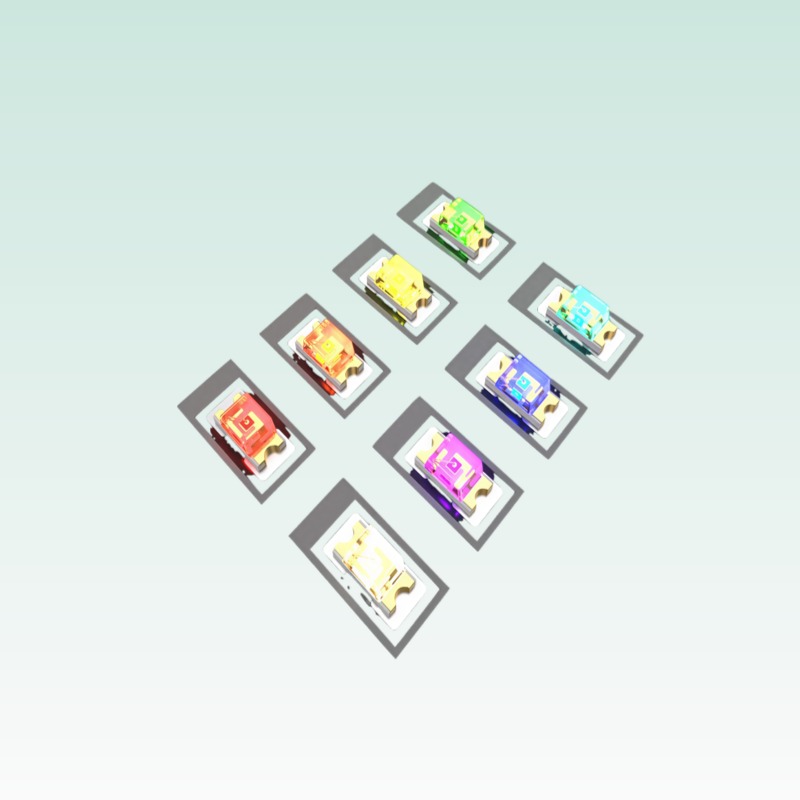
Automotive-suitable packages are drawn from the high-power ceramic and high-reliability SMD families, and the specific part number depends on the flux bin, the CRI grade and the qualification level required. The addressable and multi-colour SMD families in the J-16 group serve interior indication and accent applications, while the higher-power exterior functions draw on the ceramic high-power families. Where a part is in the qualification programme rather than fully qualified, that status is stated on the quotation.
8. Related resources and next steps
For the thermal and reliability vocabulary behind these answers, see the LED package and reliability glossary. For the electrical questions, see the LED diode and chip FAQ. For a qualification enquiry, send the application zone, the worst-case ambient and the documentation package expected, and our automotive programmes group will return a qualification status statement and a timeline.
Qualification and Testing Questions
AEC-Q102 is a matrix of stresses rather than one test; the rows below decide most qualification timelines.
| Test | Purpose | Condition sketch |
|---|---|---|
| Temperature cycling | Solder and package fatigue | -40 to +125 C, 1,000 cycles |
| HTOL | Operating life at stress | 125 C junction, 1,000 h |
| HTRB | Reverse-bias leakage stability | Max VR at high ambient |
| THB / HAST | Humidity robustness | 85 C / 85 %RH, biased |
| ESD (HBM / CDM) | Handling robustness | 2 kV HBM class targets |
| MSL / reflow simulation | Assembly survival | Per package classification |
Q16. What is the difference between grade 1 and grade 2?
Operating temperature range. Grade 1 reaches 125 C equivalent stress, grade 2 stops at 105 C. Exterior lighting is grade 1 territory; cabin ambient lighting is usually grade 2.
Q17. What does zero-failure qualification mean?
Every sample must pass every stress lot; automotive allows no statistical escapes. One bond-wire failure at 600 cycles restarts the lot after root-cause, which is why supplier change control matters.
Q18. Is PPAP required for LEDs?
At tier-1 level, yes: PPAP level 3 evidence with material declarations and process capability. Our automotive catalogue parts ship with supporting documents on request.
Thermal Derating Questions
Automotive packaging turns thermal derating into a contractual number. Five inputs set it:
| Design input | Effect | Action |
|---|---|---|
| Target Tj at end of life | Sets flux at warranty expiry | Derate 15 percent below beginning of life |
| Ambient plus solar load | Fixed by the vehicle zone | Measure behind the lens, not room temperature |
| PCB stack-up | Thermal resistance junction to back | 2 oz copper, thermal vias under the pad |
| Drive current bin | Self-heating rate | Choose the bin at Tj, not at 25 C |
| Vf spread across bins | String regulation margin | Group bins per module |
Q19. Why do red tail-lamp LEDs dim faster than white DRLs?
AlInGaP junctions lose about 0.6 percent of flux per degree versus 0.25 for InGaN white. The board that keeps white at 90 percent can drop red to 75; tail-lamp design starts from the red derating curve.
Q20. How do I validate a derating curve on my board?
Measure solder-point temperature at steady state, apply the datasheet Rth(j-sp), and confirm flux with a goniometer at temperature. A two-point check at 25 C and maximum ambient brackets the curve.
Q21. Do headlamps and interior parts share requirements?
No. Headlamps face grade 1 temperatures, vibration and photometric regulation; interior ambient lighting is grade 2 with softer flux tolerances. Mixing the two specifications inflates cost without benefit.