SMD-LED-Fehleranalyse
Umfassende Fehlerbehebung und Ursachenanalyse für oberflächenmontierte LED-Ausfälle in Leiterplattenbaugruppen – basierend auf IPC-7095, JEDEC J-STD-020 und mehr als 25 Jahren Felddaten aus industriellen und kommerziellen Anwendungen.
1. Übersicht über SMD-LED-Fehlermodi
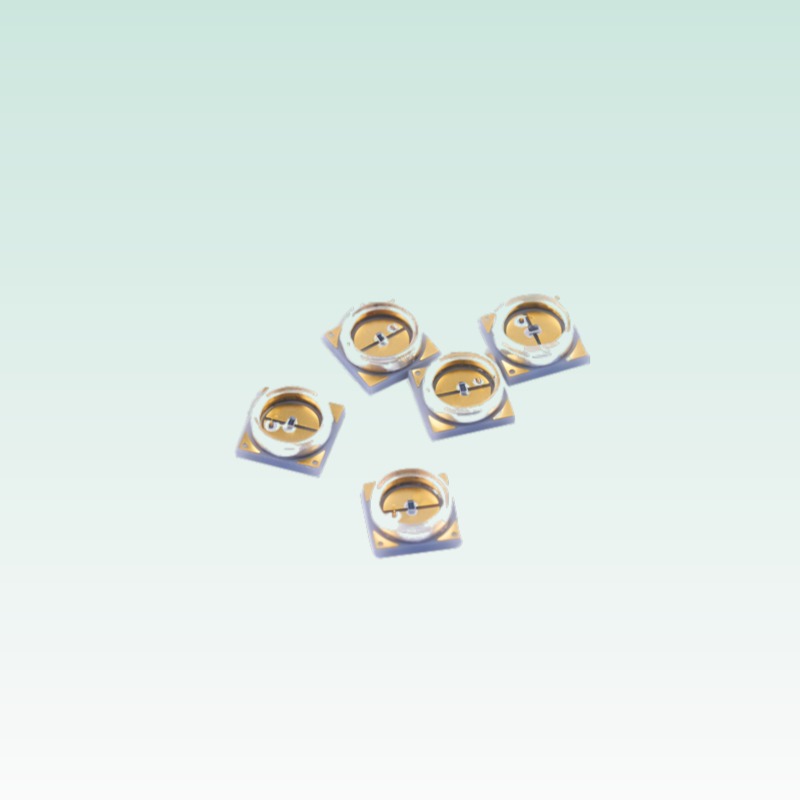
Surface-mount device (SMD) LEDs account for over 70% of LED-Pakete used in modern electronic assemblies. Their compact form factor, high luminous efficiency, and compatibility with automated reflow soldering make them the default choice for applications ranging from consumer electronics to industrial control panels. However, the very characteristics that make SMD-LEDs advantageous — small size, high power density, and leadless construction — also introduce specific failure modes that differ significantly from through-hole packages.
Industry data from major LED manufacturers and independent testing laboratories indicate that approximately 60% of SMD-LED failures in the field are attributable to solder joint issues, 20% to electrical overstress (EOS/ESD), 12% to thermal degradation, and 8% to manufacturing defects in the LED die or package itself. Understanding these failure modes is essential for PCB engineers, quality assurance teams, and field service technicians who must diagnose root causes and implement effective prevention strategies.
| Fehlerkategorie | Typische Grundursache | Feldvorkommen | Erkennungsmethode |
|---|---|---|---|
| Fehler an der Lötstelle | Kaltes Lot, unzureichende Paste, Tombstoning | ~60% | Röntgen, Querschnitt, visuelle AOI |
| EOS-/ESD-Schaden | Stoßstrom, Sperrspannung, triboelektrische Entladung | ~20% | I-V-Kurvenverfolgung, SEM-Analyse |
| Thermischer Abbau | Überhitzung der Verbindungsstelle, unzureichendes Wärmeleitpad | ~12% | Wärmebild, LM-80-Daten |
| Verpackungs-/Matrizenfehler | Chipriss, Drahtverbindungsbruch, Delaminierung | ~8% | CSAM, SEM-EDX, zerstörende Prüfung |
2. Lötstellenfehler
Solder joint reliability is the single most critical factor in SMD-LED assembly performance. The transition from tin-lead (SnPb) to lead-free solder (SAC305, SAC405) following the RoHS directive introduced higher reflow temperatures and different intermetallic compound (IMC) growth characteristics, creating new failure mechanisms that engineers must understand.
2.1 Kaltlötstellen
Cold solder joints occur when the reflow profile does not reach the liquidus temperature of the solder alloy for a sufficient time, or when oxidation on the pad or terminal prevents proper wetting. In SMD-LEDs, cold joints typically manifest as intermittent illumination — the LED may light up when pressure is applied to the package or when the board is flexed slightly. This symptom is particularly dangerous because it may pass initial QC testing but fail in the field under thermal cycling or vibration.
Wichtige Diagnoseindikatoren: Eine richtig geformte SAC305-Lötverbindung sollte einen glatten, konkaven Meniskus mit einem Kontaktwinkel von weniger als 30 Grad haben. Kalte Gelenke wirken oft körnig, matt oder haben eine konvexe Form. Eine Röntgeninspektion kann ein unzureichendes Lotvolumen oder Hohlräume aufdecken, die mehr als 25 % der Verbindungsfläche ausmachen, was nach IPC-7095 als Fehler eingestuft wird, der eine Nacharbeit erfordert.
2.2 Tombstoning
Tombstoning — where one end of the SMD-LED lifts off its pad during reflow — is caused by unequal wetting forces on the two terminals. This is particularly common in small SMD packages such as 0402 (1005 metric) and 0603 (1608 metric), where the component mass is low relative to the surface tension of molten solder. Factors contributing to tombstoning include uneven pad sizes, asymmetric copper thermal mass on the two pads, and non-symmetric stencil aperture designs.
Queendom’s production data from over 2 million SMD-LED placements shows that tombstoning rates can be reduced from 0.3% to below 0.05% by implementing three controls: (1) matching pad copper area on both terminals within 10%, (2) using a Type 4 solder paste with 20-mil stencil thickness for 0402 packages, and (3) optimizing the reflow profile ramp rate to 1.5–2.5 degrees/second through the liquidus transition zone.
2.3 Hohlräume in Lötstellen
Solder voids — trapped gas pockets within the solder joint — are a significant concern for hohe Leistung SMD-LEDs that use thermal pads for heat dissipation. IPC-7095 specifies that voiding in thermal pad solder joints should not exceed 30% of the pad area. Excessive voiding increases thermal resistance, causing the junction temperature to rise and accelerating degradation through the Arrhenius equation (every 10 degrees Celsius increase halves the LED lifetime).
3. Elektrische Überlastung (EOS) und ESD
Elektrische Überlastung ist die zweithäufigste Ursache für Ausfälle von SMD-LEDs. EOS-Ereignisse treten auf, wenn die LED selbst für sehr kurze Zeit Strom- oder Spannungspegeln ausgesetzt ist, die ihre maximalen Nennwerte überschreiten. Im Gegensatz zur allmählichen Verschlechterung sind EOS-Schäden typischerweise katastrophal und irreversibel.
3.1 Schäden durch Rückspannung
SMD-LEDs have a low reverse breakdown voltage, typically 5 volts maximum. In circuits where reverse voltage spikes occur — such as inductive load switching, hot-plug events, or signal line ringing — the LED junction can be damaged even if the forward current is within spec. The damage manifests as increased reverse leakage current, reduced forward luminous output, and eventual short-circuit failure.
Prevention: Install a reverse-parallel protection diode (e.g., 1N4148 for signal applications, Schottky diode for power applications) across the LED. For multiplexed displays, ensure the scanning circuit’s off-time reverse voltage does not exceed the LED’s Vr rating.
3.2 Schäden durch Stromstöße
Current surges from power supply turn-on transients, load switching, or ESD events can cause bond wire fusing or die-level electromigration. In hohe Leistung SMD-LEDs (such as 3535, 5050, 5630 packages), the bond wires are typically 1.0–1.5 mil gold wire, which can carry approximately 1–3 amps for short durations before fusing. However, repeated sub-fusing surges can cause cumulative damage that reduces light output and shifts the chromaticity coordinates.
4. Thermischer Abbau
Wärmemanagement is critical for SMD-LED longevity. The junction temperature (Tj) of an SMD-LED is determined by the ambient temperature, the thermal resistance of the package (Rth j-a or Rth j-s), und die power dissipation. For every 10 degrees Celsius increase in junction temperature, the LED’s L70 lifetime is approximately halved according to LM-80 test data extrapolated via TM-21.
| Package | Rth (j-s) °C/W | Max. Tj (°C) | Typische Leistung (W) | Empfohlenes Pad |
|---|---|---|---|---|
| 2835 | 35–45 | 120 | 0.5 | 25 mm² Kupfer |
| 3030 | 30–40 | 120 | 0.5–1.0 | 30 mm² Kupfer |
| 3535 | 15–25 | 150 | 1.0–3.0 | 50 mm² Wärmeleitpad |
| 5050 | 20–30 | 120 | 0.8–1.2 | 40 mm² Kupfer |
5. Fallstudie: SMD-LED-Ausfall in industrieller Schalttafel
Application: Statusanzeige-LEDs an SPS-E/A-Modulen in einer Stahlwerksumgebung
Fehlermodus: Intermittierendes Aufleuchten und eventueller Leerlauffehler bei 0603 SMD-Anzeige-LEDs nach 8–12 Monaten Betrieb
Ursachenanalyse: Cross-sectioning of failed LEDs revealed solder joint cracking at the cathode terminal. The crack propagated from the pad edge through the solder meniscus, creating a high-resistance intermittent connection that eventually failed completely. The root cause was identified as coefficient of thermal expansion (CTE) mismatch between the FR-4 substrate (CTE ~14 ppm/°C) und die SMD-LED ceramic substrate (CTE ~6 ppm/°C), combined with ambient temperature cycling from 15°C to 55°C in the control cabinet.
Solution: (1) Redesigned the PCB pad layout to include thermal relief connections, reducing mechanical stress on the solder joint. (2) Switched from SAC305 to SAC-Bi solder paste with 3% Bi content, which provides better fatigue resistance in thermal cycling. (3) Applied conformal coating (AR type) to the assembled board for additional mechanical support. After implementing these changes, field failures dropped by 92% over a 12-month observation period.
6. Präventionsstrategien und Auswahlrichtlinien
Basierend auf den oben genannten Fehleranalysedaten sollten die folgenden Präventionsstrategien in der Entwurfs-, Herstellungs- und Feldeinsatzphase umgesetzt werden:
- Entwurfsphase: Select LED-Pakete with thermal resistance values appropriate for the application’s power dissipation and ambient temperature. Design PCB pads per IPC-7351 guidelines, ensuring balanced copper on both terminals. Include current-limiting resistors with appropriate power ratings, and consider TVS diodes for transient protection in harsh electrical environments.
- Herstellungsphase: Implement AOI (Automated Optical Inspection) with 2D and 3D inspection for every SMD-LED placement. Use X-ray inspection for hohe Leistung packages with thermal pads. Monitor reflow profile conformance using a profiling instrument on every batch change. Control solder paste storage conditions (temperature: -5 to 10°C, humidity: <10% RH).
- Feldeinsatz: Ensure the operating environment does not exceed the LED’s rated junction temperature. In high-vibration applications, use underfill or conformal coating. Implement ESD protection at the enclosure level, particularly in dry environments where relative humidity is below 30%.
7. FAQ
F: Wie hoch ist die typische L70-Lebensdauer einer SMD-LED, die bei einer Sperrschichttemperatur von 85 °C betrieben wird?
A: Basierend auf LM-80-Testdaten für die meisten SMD-LEDs namhafter Hersteller beträgt die L70-Lebensdauer bei 85 °C Tj bei Betrieb mit Nennstrom typischerweise 36.000–50.000 Stunden. Bei 105 °C Tj sinkt diese auf etwa 15.000–20.000 Stunden.
F: Kann eine ausgefallene SMD-LED andere Komponenten auf derselben Platine beschädigen?
A: Ja. Eine LED, die aufgrund eines Kurzschlusses ausfällt, kann übermäßigen Strom ziehen und möglicherweise den Strombegrenzungswiderstand, den Treiber-IC oder die Leiterbahnen auf der Leiterplatte beschädigen. Bauen Sie für kritische Anwendungen immer eine Sicherung oder ein Strombegrenzungsgerät in die LED-Treiberschaltungen ein.
F: Wie hoch ist der maximal zulässige Hohlraumanteil in SMD-LED-Lötverbindungen?
A: Gemäß IPC-7095 sollten Hohlräume in Lötstellen für elektrische Verbindungen nicht mehr als 25 % der Verbindungsfläche ausmachen. Bei Wärmeleitpad-Lötverbindungen (verwendet in Hochleistungs-SMD-LEDs) liegt die Grenze bei 30 %. Bei einer Entleerung oberhalb dieser Grenzwerte ist eine Nacharbeit erforderlich.
8. Verwandte Ressourcen
- Leitfaden zum Wärmemanagement-Design für LED-Anwendungen — detaillierte thermische Berechnungsmethoden und Kühlkörperdesign
- LM-80-Tests und LED-Lebensdauerschätzung — Standards für Zuverlässigkeitstests und Dateninterpretation
- Leitfaden zur Auswahl von SMD-LED-Paketen — Wählen Sie das richtige SMD-Gehäuse für Ihre Anwendung
- SMD-LED-Datenblätter — Laden Sie detaillierte Spezifikationen für alle SMD-Serien herunter
9. Herstellungsprozesskontrollen für die Zuverlässigkeit von SMD-LEDs
Beyond design-stage prevention, manufacturing process controls play a critical role in SMD-LED long-term reliability. Statistical process control (SPC) charts should be maintained for key parameters including solder paste deposition volume, reflow temperature profile conformity, and post-reflow coplanarity. A capable manufacturing process maintains a Cpk (process capability index) of 1.33 or higher for each of these parameters, ensuring that the statistical distribution of solder joint quality is well within specification limits.
Incoming quality control for SMD-LED-Pakete should include: (1) visual inspection per AEC-Q200 for mechanical damage, (2) MSL (Moisture Sensitivity Level) verification to ensure packages are stored and handled within their rated moisture exposure limits, (3) reel-to-reel photometric screening to verify luminous flux and chromaticity consistency within each reel, and (4) periodic destructive physical analysis (DPA) sampling to verify die attach quality, wire bond geometry, and encapsulation integrity.
For automotive and safety-critical applications, additional controls per IATF 16949 include PPAP (Production Part Approval Process) documentation, 8D problem-solving methodology for any field failures, and traceability from individual LED-Pakete back to the wafer production lot. This traceability enables rapid root cause analysis when field failures occur, allowing corrective actions to be implemented across all potentially affected production lots.
10. Neue Fehlermodi in Mini-LED- und Micro-LED-Gehäusen
As the LED industry transitions toward mini-LED (100–300 micron pitch) and micro-LED (less than 100 micron pitch) packages for high-density displays, new failure modes are emerging that PCB engineers should be aware of. These include: (1) mass transfer bonding defects where the tiny LED-Chips are transferred from the source wafer to the destination substrate, with transfer yields currently in the 99.9% range leaving a small but nonzero population of missing or misaligned LEDs, (2) increased sensitivity to current crowding effects in very small active area devices, and (3) optical crosstalk between adjacent mini-LED pixels caused by insufficient light blocking structures. While these technologies are still maturing, engineers specifying mini-LED backlights or displays should work closely with suppliers to understand the expected defect rates and failure modes.
For traditional SMD-LED-Anwendungs (0402 through 5050 packages), the failure modes and prevention strategies described in this guide remain comprehensive and applicable. The key to long-term reliability is a holistic approach that addresses thermal design, current regulation, ESD protection, solder joint quality, and environmental protection simultaneously — no single factor alone can guarantee LED reliability, but neglecting any one factor can cause premature failure.
9. Herstellungsprozesskontrollen für die Zuverlässigkeit von SMD-LEDs
Beyond design-stage prevention, manufacturing process controls play a critical role in SMD-LED long-term reliability. Statistical process control (SPC) charts should be maintained for key parameters including solder paste deposition volume, reflow temperature profile conformity, and post-reflow coplanarity. A capable manufacturing process maintains a Cpk (process capability index) of 1.33 or higher for each of these parameters, ensuring that the statistical distribution of solder joint quality is well within specification limits.
Incoming quality control for SMD-LED-Pakete should include: (1) visual inspection per AEC-Q200 for mechanical damage, (2) MSL (Moisture Sensitivity Level) verification to ensure packages are stored and handled within their rated moisture exposure limits, (3) reel-to-reel photometric screening to verify luminous flux and chromaticity consistency within each reel, and (4) periodic destructive physical analysis (DPA) sampling to verify die attach quality, wire bond geometry, and encapsulation integrity.
For automotive and safety-critical applications, additional controls per IATF 16949 include PPAP (Production Part Approval Process) documentation, 8D problem-solving methodology for any field failures, and traceability from individual LED-Pakete back to the wafer production lot. This traceability enables rapid root cause analysis when field failures occur, allowing corrective actions to be implemented across all potentially affected production lots.
10. Neue Fehlermodi in Mini-LED- und Micro-LED-Gehäusen
As the LED industry transitions toward mini-LED (100-300 micron pitch) and micro-LED (less than 100 micron pitch) packages for high-density displays, new failure modes are emerging that PCB engineers should be aware of. These include: (1) mass transfer bonding defects where the tiny LED-Chips are transferred from the source wafer to the destination substrate, with transfer yields currently in the 99.9% range leaving a small but nonzero population of missing or misaligned LEDs, (2) increased sensitivity to current crowding effects in very small active area devices, and (3) optical crosstalk between adjacent mini-LED pixels caused by insufficient light blocking structures. While these technologies are still maturing, engineers specifying mini-LED backlights or displays should work closely with suppliers to understand the expected defect rates and failure modes.
For traditional SMD-LED-Anwendungs (0402 through 5050 packages), the failure modes and prevention strategies described in this guide remain comprehensive and applicable. The key to long-term reliability is a holistic approach that addresses thermal design, current regulation, ESD protection, solder joint quality, and environmental protection simultaneously. No single factor alone can guarantee LED reliability, but neglecting any one factor can cause premature failure. Engineers are encouraged to use Queendom’s SMD-LED reliability testing data and application notes as design references, and to contact our engineering team for application-specific reliability guidance.
9. Herstellungsprozesskontrollen für die Zuverlässigkeit von SMD-LEDs
Beyond design-stage prevention, manufacturing process controls play a critical role in SMD-LED long-term reliability. Statistical process control (SPC) charts should be maintained for key parameters including solder paste deposition volume, reflow temperature profile conformity, and post-reflow coplanarity. A capable manufacturing process maintains a Cpk (process capability index) of 1.33 or higher for each of these parameters, ensuring that the statistical distribution of solder joint quality is well within specification limits.
Incoming quality control for SMD-LED-Pakete should include: (1) visual inspection per AEC-Q200 for mechanical damage, (2) MSL (Moisture Sensitivity Level) verification to ensure packages are stored and handled within their rated moisture exposure limits, (3) reel-to-reel photometric screening to verify luminous flux and chromaticity consistency within each reel, and (4) periodic destructive physical analysis (DPA) sampling to verify die attach quality, wire bond geometry, and encapsulation integrity.
For automotive and safety-critical applications, additional controls per IATF 16949 include PPAP (Production Part Approval Process) documentation, 8D problem-solving methodology for any field failures, and traceability from individual LED-Pakete back to the wafer production lot. This traceability enables rapid root cause analysis when field failures occur, allowing corrective actions to be implemented across all potentially affected production lots.
10. Neue Fehlermodi in Mini-LED- und Micro-LED-Gehäusen
As the LED industry transitions toward mini-LED (100-300 micron pitch) and micro-LED (less than 100 micron pitch) packages for high-density displays, new failure modes are emerging that PCB engineers should be aware of. These include: (1) mass transfer bonding defects where the tiny LED-Chips are transferred from the source wafer to the destination substrate, with transfer yields currently in the 99.9% range leaving a small but nonzero population of missing or misaligned LEDs, (2) increased sensitivity to current crowding effects in very small active area devices, and (3) optical crosstalk between adjacent mini-LED pixels caused by insufficient light blocking structures. While these technologies are still maturing, engineers specifying mini-LED backlights or displays should work closely with suppliers to understand the expected defect rates and failure modes.
For traditional SMD-LED-Anwendungs (0402 through 5050 packages), the failure modes and prevention strategies described in this guide remain comprehensive and applicable. The key to long-term reliability is a holistic approach that addresses thermal design, current regulation, ESD protection, solder joint quality, and environmental protection simultaneously. No single factor alone can guarantee LED reliability, but neglecting any one factor can cause premature failure. Engineers are encouraged to use Queendom SMD-LED reliability testing data and application notes as design references, and to contact our engineering team for application-specific reliability guidance.